

How has DUPUY helped with dust extraction in fertilizer production?
Mineral Fertilizer Production: Dust Control in Industrial Processes
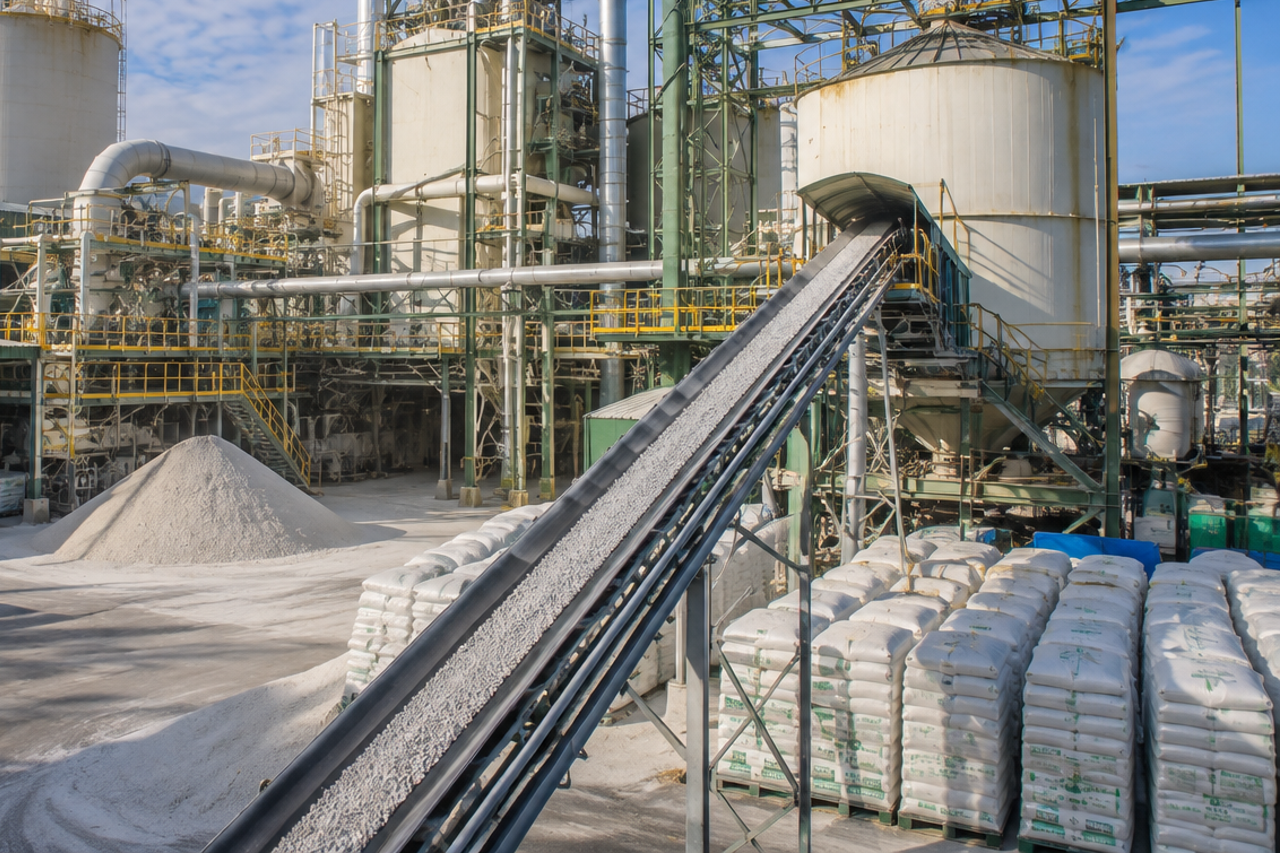
In the mineral fertilizer industry, the handling and processing of raw materials can generate significant amounts of dust. These particles tend to disperse throughout production areas, making it necessary to capture them effectively right where they are generated.
This was the situation faced by a company located in Poland, which needed a dust collection system connected to its production equipment.
The process involved several emission points distributed along the line, each of which required adequate ventilation to limit the dispersion of material into the surrounding environment.
An additional source of complexity was the ATEX Zone 22 classification of the production area, which required special attention to managing the risks associated with potentially explosive atmospheres.
The customer also needed to control odors in the intake air and to install protective devices capable of preventing the spread of a potential explosion through the piping.
The goal was therefore to develop a centralized solution that would combine localized exhaust, filtration, and safety measures tailored to the system’s specifications.
Key Project Data
8
Simultaneous Extraction Points
A single centralized system captures dust from eight points along the line, eliminating the need to install a separate dust collector for each workstation
2-IN-1
Dust Extraction and Odor Control
Dust removal and activated carbon post-filtration integrate two air treatment functions into a single system solution.
Vacuuming dust from eight locations while ensuring emissions and safety are kept under control
The customer’s main challenge was the need to capture the dust generated during the production of mineral fertilizers at various points along the production line.
The distribution of emissions required a centralized extraction system capable of serving eight points simultaneously, ensuring effective collection of particles directly at the source.
The presence of an ATEX Zone 22-classified environment also made it necessary to adopt a configuration appropriate for the risks associated with potentially explosive atmospheres.
Specifically, the customer needed to install a device that would help prevent the spread of a potential explosion through the piping network.
Another requirement concerned the treatment of the extracted air. In addition to dust separation, the process required a system capable of reducing odors before the air was released back into the environment.
Finally, it was necessary to ensure reliable, long-term operation by limiting dust buildup on the filters and reducing the frequency of manual maintenance.
A centralized system for controlling dust, odors, and operational risks
In the production of mineral fertilizers, relying solely on periodic cleaning operations does not meet the need to control dust as it is generated.
The presence of multiple emission points called for a solution capable of operating directly within the production process, limiting the dispersion of particles before they reached the surrounding areas.
For the customer, the priority was therefore to implement a centralized vacuum system that would allow for the simultaneous management of various dust sources.
The ATEX Zone 22 classification also made it essential to incorporate specific safety devices. In particular, the piping system had to be equipped with a system designed to prevent the propagation of a potential explosion.
Odor control was another requirement. Particle filtration had to be supplemented by additional treatment of the extracted air.
The ultimate goal was to develop a comprehensive system capable of combining localized extraction, post-filtration, and automatic filter monitoring, thereby simplifying plant management and promoting operational continuity.
DUPUY DEDUST 8 ATEX Z22: Centralized dust collection system with eight suction points
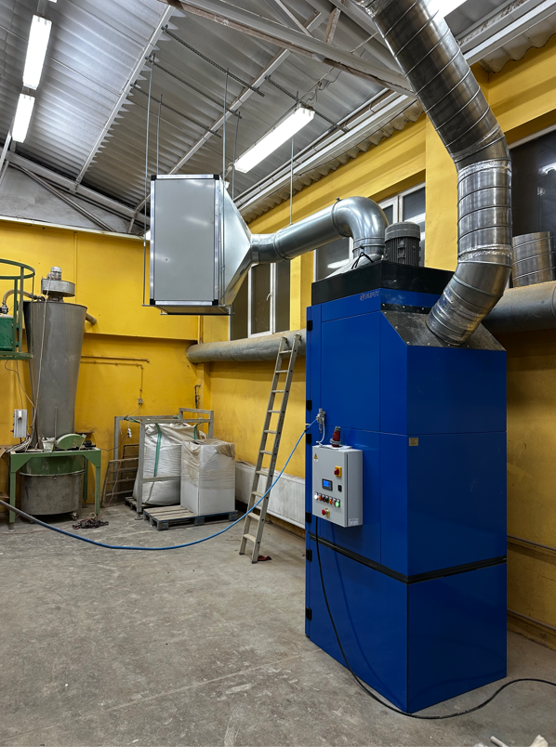
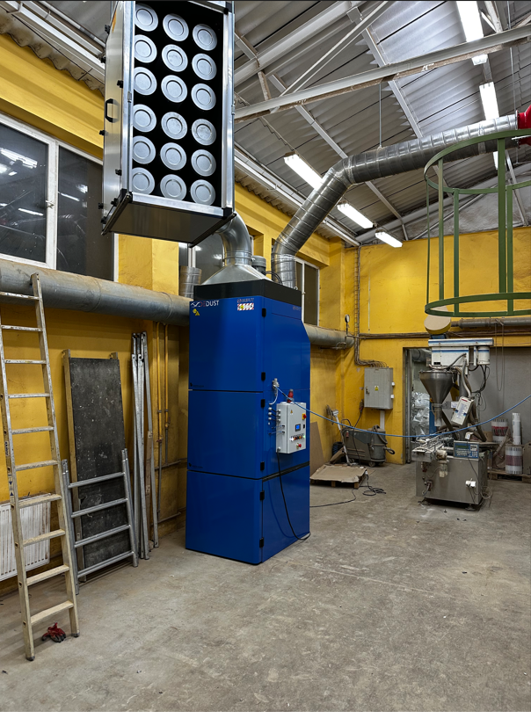
To meet the customer’s needs, DUPUY has developed a centralized dust collection system based on the DEDUST 8 ATEX Z22, designed to capture dust directly at the points where it is generated during the production of mineral fertilizers.
The system was designed to serve eight extraction points, each equipped with Ø100 mm connections. This configuration allows for distributed extraction throughout the production process, focusing the system’s operation on the various emission sources.
Downstream of the main unit, an activated carbon post-filtration stage has been installed, designed to treat the extracted air and reduce odors before it is released back into the environment.
To further enhance the system’s safety, a check valve has also been installed, designed to prevent the spread of a potential explosion through the piping.
Another key component of the solution is the automatic pneumatic filter cleaning system, which is controlled directly by the electrical control panel.
The system operates by monitoring the differential pressure ΔP: it detects when the filters are clogged and automatically initiates the cleaning cycle based on operational needs.
This approach helps maintain more consistent filtration performance over time, reducing the need for manual intervention and contributing to the system’s overall efficiency.
The combination of distributed ventilation, air treatment, and safety devices made it possible to develop a solution specifically tailored to the operating conditions at the Polish plant.
Less dust dispersion and greater control over the production process
The installation of the DEDUST 8 ATEX Z22 has enabled the customer to manage dust extraction directly during the production of mineral fertilizers through a dedicated network connected to the various emission points.
The presence of eight collection points allows for simultaneous intervention along the line, limiting the dispersion of particles in the production environment.
The inclusion of an activated carbon post-filter helps reduce odors in the extracted air, while the check valve provides an additional layer of protection against the spread of a potential explosion through the intake system.
The automatic filter cleaning system, which monitors differential pressure (ΔP), also allows for clogging to be managed based on operating conditions, reducing the need for manual intervention.
Together, these features help improve the efficiency and reliability of the dust collection system, thereby ensuring the continuity of production operations.
The main benefits achieved:
- Dust collection directly at the emission points.
- Simultaneous extraction from eight points along the production line.
- Reduction of particle dispersion in the workplace.
- Odor control through activated carbon post-filtration.
- Increased safety of the extraction system thanks to the check valve.
- Automatic monitoring of filter clogging via differential pressure (ΔP).
- Reduced need for manual filter cleaning.
- Greater continuity and efficiency of the extraction system.
This project demonstrates how a centralized system, tailored to the application’s requirements, can integrate various extraction, filtration, and safety functions into a single solution.